AXA VSC 2 - XTS50
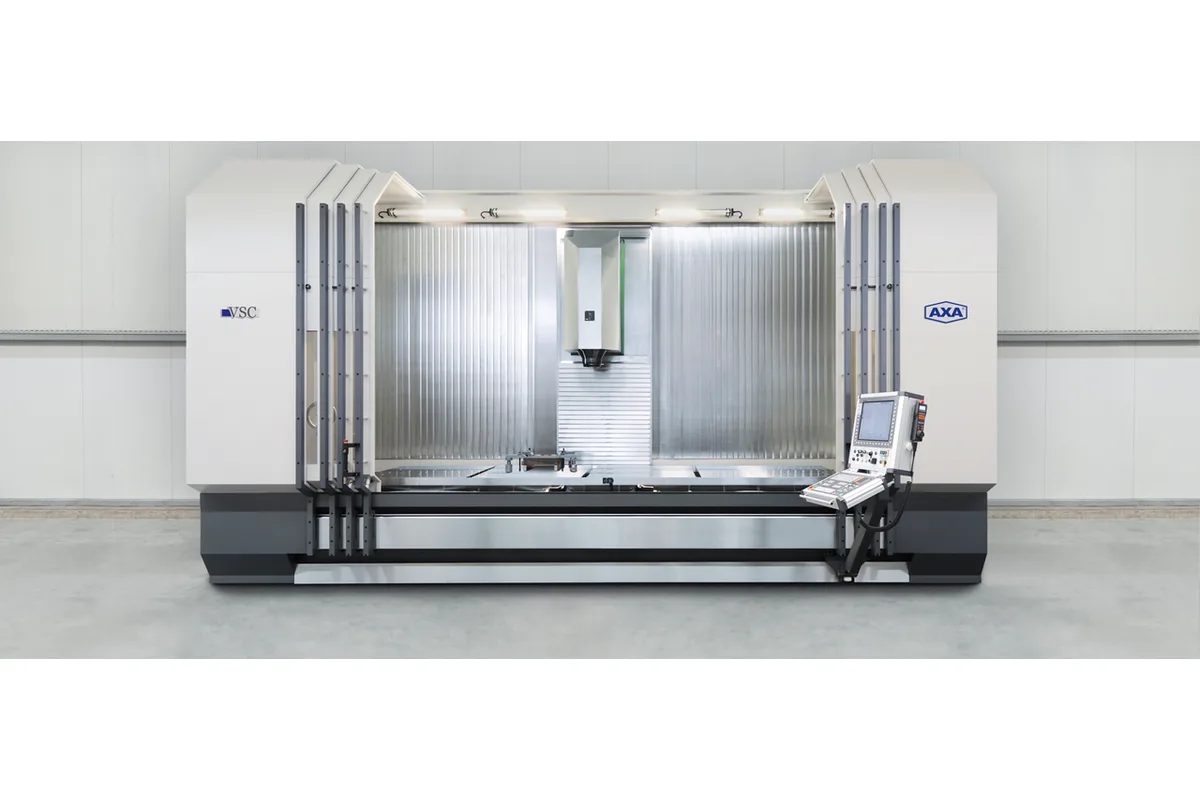
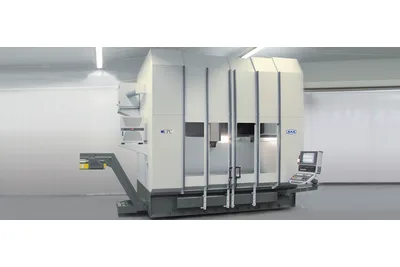
Image: axa-maschinenbau.de, AXA
Key Specifications
Max Spindle
Spindle Taper
Tool Capacity
Table Size
Spindle Power
Accuracy
How much does the AXA VSC 2 - XTS50 cost?
Price estimate
We do not have a price for the AXA VSC 2 - XTS50 that we can stand behind, so we show no number. Configuration, options and installation move the final price a long way: a quote is the reliable figure.
Overview
Take the VSC 2 frame and fit an SK 50 spindle: that is the AXA VSC 2 - XTS50. Its travels are unchanged at 600 mm (23.6 in) in Y and 850 mm (33.5 in) in Z, with X built to order from 1,760 mm to 9,000 mm, but the standard drive no. 131 puts 286 Nm and 45 kW at 40% DC behind the cutter. The VSC 2 - XTS, the SK 40 version of this frame, has 143 Nm.
The heavier taper changes the tooling side of the machine. Magazine pockets are larger, so a tool can be 110 mm in diameter with every pocket filled and 180 mm with free adjacent pockets. The price is capacity and time. The XTS magazine starts at 26 pockets and extends to 156 where the VSC 2 - XTS reaches 216, and a tool change takes approx. 7 s.
Only one optional drive is listed, no. 133, with 355 Nm and 56 kW. Both drives turn 4,000 rpm as standard and up to 9,000 rpm as an option, so this is a machine for torque, not for small high-speed tools. Tool holders are SK 50 to DIN ISO 7388-1 AD / DIN ISO 7388-3 AD, with BT 50, HSK A100 or C8 optional.
T-slots are 18 mm wide where the VSC 2 - XTS has 14 mm, on the same four-slot table rated at 1,000 kg/m². Feed force stays at 9,000 N and rapids at 40/40/30 m/min. Buyers who need more thrust and a stiffer drive train should look at the VSC 50 - XTS, which is rated at 20,000 N.
Full Specifications
| Parameter | Value |
|---|---|
| X Axis Travel | 1,760 - 9,000 mm (69.3 - 354.3 in) |
| Pendulum Travel Optional | (X-axis - 500) / 2 mm |
| Y Axis Travel | 600 mm (23.6 in) |
| Z Axis Travel | 850 mm (33.5 in) |
| Distance Spindle Nose to Table | 180 - 1,030 mm (7.1 - 40.6 in) |
| Table Size | (X-axis + 400) x Y-axis mm |
| T-Slot Width | 18 mm H9 (reference slot H7) |
| T Slot Spacing | 160 mm (6.3 in) |
| T Slot Count | 4 |
| Max Table Load | 1,000 kg/m² (205 lb/ft²) |
| Rapid Traverse Xyz | 40/40/30 m/min (1,575/1,575/1,181 ipm) in X/Y/Z |
| Max Feed Force | 9,000 N (2,023 lbf) |
| Spindle Drive Standard | No. 131 |
| Spindle Drives Optional | No. 133 |
| Max Spindle Speed | 4,000 rpm; optional up to 9,000 rpm (standard drive no. 131) |
| Spindle Torque | 286 Nm (211.0 lb-ft) max. at 40% DC (standard drive no. 131) |
| Spindle Motor Power | 45 kW (60.3 hp) max. at 40% DC (standard drive no. 131) |
| Optional Spindle Drive 133 | 4,000 rpm (optional up to 9,000 rpm), 355 Nm (261.8 lb-ft), 56 kW (75.1 hp) max. at 40% DC |
| Spindle Taper | SK 50 (DIN ISO 7388-1 AD / DIN ISO 7388-3 AD); optional BT 50, HSK A100, C8 |
| Tool Capacity | 26; optional expandable up to 156 (e.g. 3 fully equipped towers) |
| Max Tool Diameter (full magazine) | 110 mm (4.3 in); 180 mm (7.1 in) with free adjacent pockets |
| Max Tool Length | 400 mm (15.7 in) |
| Tool Change Time | approx. 7 s |
| Positioning Accuracy | ± 0.015 mm per 1,000 mm per axis X/Y/Z; optional ± 0.0075 mm |
| Repeatability | ± 0.005 mm |
Specifications sourced from axa-maschinenbau.de — verified 2026-10-05
Strengths & Limitations
Strengths
- SK 50 spindle with 286 Nm and 45 kW at 40% DC as standard
- Optional drive no. 133 with 355 Nm and 56 kW
- Tools up to 110 mm in diameter, or 180 mm with free adjacent pockets
- Same compact cross-section as the SK 40 model: 600 mm of Y, 850 mm of Z
- Rapid traverse of 40/40/30 m/min is kept despite the heavier spindle
Limitations
- Spindle speed is 4,000 rpm as standard and 9,000 rpm at most
- The magazine extends to 156 pockets, fewer than the 216 of the VSC 2 - XTS
- Tool change takes approx. 7 s
- Feed force is 9,000 N, less than half the 20,000 N of the VSC 50 - XTS
Best For
Frequently Asked Questions
01
The spindle and everything sized to it. The VSC 2 - XTS50 has an SK 50 taper, 286 Nm and 45 kW as standard, 18 mm T-slots, 26 to 156 tool pockets and a tool change of approx. 7 s. The VSC 2 - XTS has SK 40, 143 Nm and 30 kW, 14 mm T-slots, 22 to 216 pockets and approx. 5 s. Travels are identical.
02
Both listed drives, no. 131 and no. 133, have a speed range of 4,000 rpm and can be ordered with up to 9,000 rpm. Torque is 286 Nm or 355 Nm and power 45 kW or 56 kW, each stated at 40% DC.
03
Up to 110 mm (4.3 in) in diameter with a full magazine and 180 mm (7.1 in) with free adjacent pockets, at a length of up to 400 mm (15.7 in). The data sheet does not state a maximum tool weight, so ask AXA before planning heavy boring tools.
04
Yes, as an option. AXA gives the pendulum travel as (X-axis - 500) / 2 mm, so each of the two zones gets half of what remains after 500 mm is taken off the X travel. The casing is designed as a closed working area in pendulum mode as well.
More from AXA
Other Vertical Machining Centers (VMC)
Haas VF-6/40
Vision Wide NF-5026 / NF-5033