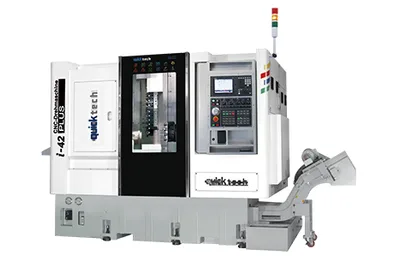
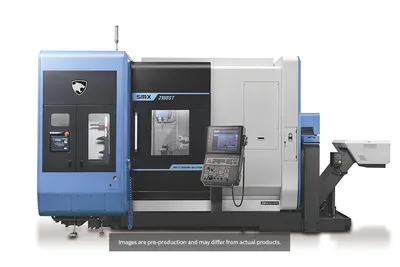
Quicktech i-42 Ultimate
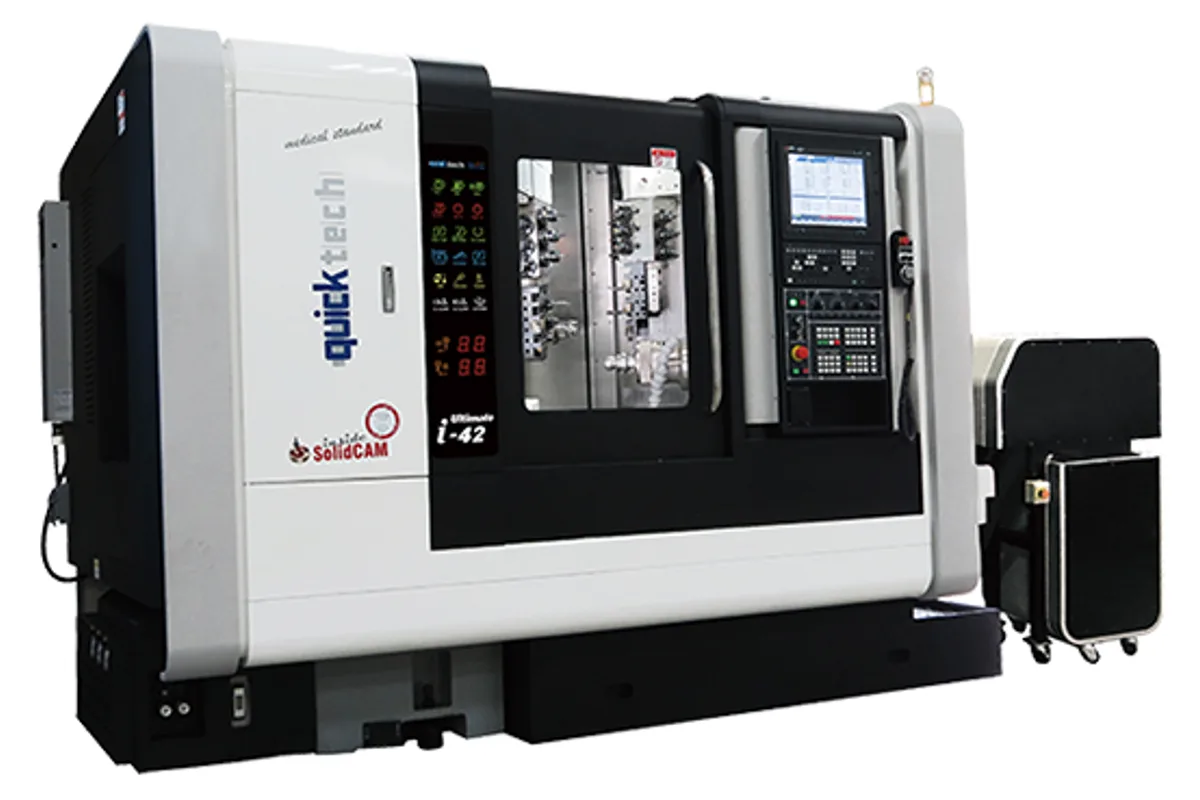
Image: quicktech.com.tw, Quicktech
Key Specifications
Max Spindle
Rapid Traverse
Spindle Power
Max Turn Length
Repeatability
control
How much does the Quicktech i-42 Ultimate cost?
Price estimate
We do not have a price for the Quicktech i-42 Ultimate that we can stand behind, so we show no number. Configuration, options and installation move the final price a long way: a quote is the reliable figure.
Overview
The Quicktech i-42 Ultimate is a twin-spindle gang-tooling lathe with two independent tool systems, each with its own X, Y and Z axes and its own block of live tools. Bar capacity is 42 mm (1.7 in), with 65 mm (2.6 in) as an option, and the maker counts 10 axis and 4 spindles in the designation. It is the top of the i-42 line: the i-42 Twin shares the two work spindles but gives the second system a Z axis only.
What the second full axis group buys is overlap. The first system travels 150 / 410 / 250 mm (5.9 / 16.1 / 9.8 in) in X1/Y1/Z1 and the second 450 / 380 / 300 mm (17.7 / 15.0 / 11.8 in) in X2/Y2/Z2, so the sub-spindle side can be positioned in X as well as Z and both ends of a part can be machined at once. The motorized tool row reads T1=12 / T2=12. Each live tool takes an ER-20 collet and runs to 4,000 rpm, with drilling up to 12.0 mm (0.5 in) and tapping to M10xP1.5.
The B axis is listed at 360°, and the maker's page shows the machine in three arrangements: dual B-axis, single B-axis and no B-axis. Ask which one a quotation covers, because the tilting milling head is what makes angled drilling possible without special holders.
The main spindle is an 11.0 kW (14.8 hp) servo spindle with an A2-5 nose and 4,000 rpm as standard; 6,000 rpm is the listed option. The sub-spindle takes 30 mm (1.2 in) bar on 3.7 kW (5.0 hp). Quicktech states that the two spindles synchronize to an accuracy of 0.02 degrees while in motion for part transfer and parting off. Castings are FC35 Meehanite, the control is a Mitsubishi M830S, and the machine weighs 5,600 kg (12,346 lb).
Full Specifications
| Parameter | Value |
|---|---|
| CNC Control | Mitsubishi M830S |
| Max Turning Diameter | 100 mm (3.9 in) |
| Bar Capacity | 42 mm (1.7 in); option 65 mm (2.6 in) |
| Max Turning Length | 230 mm (9.1 in) |
| Collet Chuck Type | KK5-173E42B; option KK6-185E60B |
| Spindle Nose | A2-5; option A2-6 |
| Spindle Bore | 43 mm (1.7 in); option 66 mm (2.6 in) |
| Max Spindle Speed | 4,000 rpm; option 6,000 rpm |
| Sub Spindle Max Turning Diameter | 100 mm (3.9 in) |
| Sub Spindle Bar Capacity | 30 mm (1.2 in) |
| Sub Spindle Max Turning Length | 100 mm (3.9 in) |
| Sub Spindle Collet Chuck Type | KK5-173E42B |
| Sub Spindle Nose | A2-5 |
| Sub Spindle Bore | 31 mm (1.2 in) |
| Sub Spindle Speed | 4,000 rpm; option 6,000 rpm |
| C Axis Least Command Unit | 0.001° |
| C Axis Positioning Accuracy | 0.02° |
| X1 Y1 Z1 Axis Travel | 150 / 410 / 250 mm (5.9 / 16.1 / 9.8 in) |
| X2 Y2 Z2 Axis Travel | 450 / 380 / 300 mm (17.7 / 15.0 / 11.8 in) |
| Rapid Traverse Rate | 30 m/min (1,181 ipm) |
| Repeatability | 0.005 mm (0.0002 in) |
| Spindle Motor Power | Servo Spindle 11.0 kW (14.8 hp) |
| Sub Spindle Power | Servo Spindle 3.7 kW (5.0 hp) |
| X1 Y1 Z1 Axis Motor | AC Servo 1.5 kW (2.0 hp) |
| X2 Y2 Z2 Axis Motor | AC Servo 1.5 kW (2.0 hp) |
| Motorized Tool Motor | AC Servo 1.5 kW (2.0 hp) |
| OD ID Tools Main Spindle | 6 / 5 |
| Tool Shank Size | □ 20 mm |
| Drill Holder Size Main | ER-20 / Ø20 mm |
| Drill Holder Size Sub | ER-20 / Ø20 mm |
| Motorized Tools | T1=12 / T2=12 |
| B Axis Range | 360° |
| Driven Tool Speed | 4,000 rpm |
| Motorized Tool Collet | ER-20 |
| Max Drilling Diameter | 12.0 mm (0.5 in) |
| Max Tapping Capacity | M10xP1.5 |
| Hydraulic Pump Tank Capacity | 1 HP / 40 L + 25 L |
| Hydraulic Pressure Flow | 30 kg/cm² / 12 L/min |
| Coolant Pump | TPH4T5K, 5 bar, 75 L/min |
| Coolant System Hydraulic Pump | 2 HP + SF-30C, 25 bar, 30 L/min |
| Coolant Tank Capacity | 240 L |
| Machine Dimensions | 3,500 (2,900) / 1,900 / 1,950 mm (137.8 (114.2) / 74.8 / 76.8 in), length / width / height |
| Machine Weight | 5,600 kg (12,346 lb) |
Specifications sourced from quicktech.com.tw — verified 2026-10-05
Strengths & Limitations
Strengths
- Two complete tool systems: X1/Y1/Z1 of 150 / 410 / 250 mm (5.9 / 16.1 / 9.8 in) and X2/Y2/Z2 of 450 / 380 / 300 mm (17.7 / 15.0 / 11.8 in)
- Motorized tools listed as T1=12 / T2=12, each on an ER-20 collet at up to 4,000 rpm
- B axis of 360° on the tilting milling head for angled drilling and tapping
- Spindles synchronize to 0.02 degrees in motion for part transfer and parting off, according to the maker
- High-pressure coolant pump of 25 bar, 30 L/min alongside the 5 bar, 75 L/min pump, with a 240 L tank
Limitations
- The sub-spindle takes 30 mm (1.2 in) bar and 100 mm (3.9 in) of turning length, well under the main spindle's capacity
- Live tools are limited to 12.0 mm (0.5 in) drilling and M10xP1.5 tapping
- Standard spindle speed is 4,000 rpm; 6,000 rpm is an option
- The maker shows versions with dual, single and no B-axis, so the B axis cannot be assumed on every machine
Best For
Frequently Asked Questions
01
Both have a main and a sub-spindle. On the i-42 Ultimate the second tool system has full X2/Y2/Z2 travel of 450 / 380 / 300 mm (17.7 / 15.0 / 11.8 in) and its own 12 motorized tools (T1=12 / T2=12). The i-42 Twin's table gives the second system a Z2 travel only and lists 12 motorized tools in total. The control also differs: Mitsubishi M830S here, Mitsubishi M80 on the i-42 Twin.
02
42 mm (1.7 in) through the main spindle as standard, with a 43 mm (1.7 in) bore and an A2-5 nose. The option is 65 mm (2.6 in) bar with a 66 mm (2.6 in) bore and an A2-6 nose. The sub-spindle takes 30 mm (1.2 in) bar. Maximum turning length is 230 mm (9.1 in) on the main spindle and 100 mm (3.9 in) on the sub-spindle.
03
The table lists motorized tools as T1=12 / T2=12, driven by an AC Servo 1.5 kW (2.0 hp) motor at up to 4,000 rpm. The collet is ER-20, maximum drilling diameter is 12.0 mm (0.5 in) and maximum tapping capacity is M10xP1.5. The B axis is listed at 360°, and the maker describes the milling head as tilting with 12 motorized tools.
04
The table gives a least command unit of 0.001° and a positioning accuracy of 0.02° for the C axis. Repeated positioning accuracy of the linear axes is listed as 0.005 mm (0.0002 in), and rapid feed is 30 m/min (1,181 ipm).
More from Quicktech
Other Mill-Turn / Multi-Tasking Machines
Okuma MULTUS U3000

Hurco TMX8MYSi
Stama MT 733 Twin
Willemin-Macodel 508MT2
DN Solutions SMX 5100 L