LVD Strippit PX-L
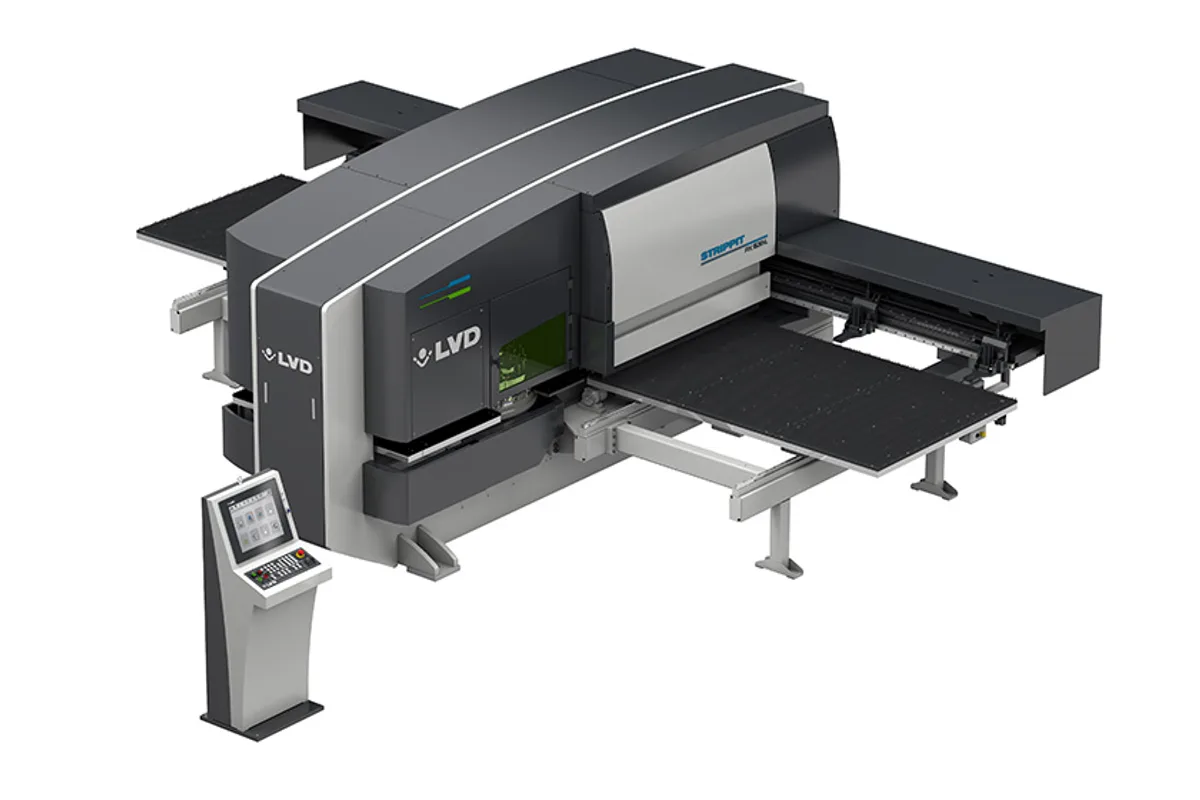
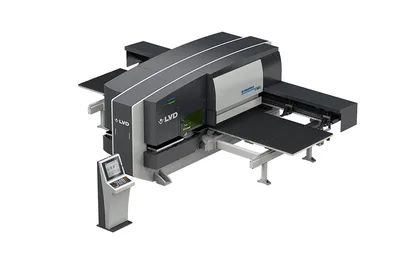
Image: lvdgroup.com, LVD
Key Specifications
Repeatability
punching force
max sheet thickness
punching accuracy
max hit rate 1mm
max hit rate 25mm
How much does the LVD Strippit PX-L cost?
Price estimate
We do not have a price for the LVD Strippit PX-L that we can stand behind, so we show no number. Configuration, options and installation move the final price a long way: a quote is the reliable figure.
Overview
The LVD Strippit PX-L combines a single-head punch press with a 4-kW fiber laser in one machine. The punching side is the Strippit PX head: 200 kN, 20 direct-drive indexable stations for tools up to 90 mm, every tool rotating a full 360 degrees. The laser cuts outer contours and intricate inner contours and can etch.
The logic of a combination machine is that each process does what it is good at. Standard holes, forms, taps and bends come from tooling at 910 HPM at 1 mm pitch; shapes with no matching tool, and the outside profile, are laser cut. A part with louvers, tapped holes and a curved outline leaves the machine complete, and the outline is a laser edge instead of a nibbled one. LVD states that a full-size workpiece of 3050 x 1525 mm is cut and punched without repositioning. The specification table gives the nominal worksheet as 3,050 x 1,550 mm (120.1 x 61.0 in).
Feed clearance is 80 mm (3.1 in), and forming heights reach 75 mm, so the forming ability of the stand-alone PX is kept. Punching thickness is up to 6.35 mm (0.25 in). Tool change takes 3 - 6.5 sec., longer than on the Strippit PX-1530 at 1 to 5 sec., and the hit rate at 25.4 mm pitch is 440 HPM.
Two chutes take parts away: a 500 x 525 mm (19.7 x 20.7 in) work chute, and a 406 mm x 1524 mm chute for laser-cut parts and scrap. Three CNC clamps relocate automatically, and the brush table carries up to 150 kg (331 lb) at reduced speed.
Adding the laser roughly doubles the listed average power consumption, 14.3 kW here against 6.7 kW for the Strippit PX-1530. LVD's table gives no laser cutting thicknesses or speeds for the machine, so those have to be requested. Control is the Touch-PL, programmed through CADMAN-PL.
Full Specifications
| Parameter | Value |
|---|---|
| Punching Force | 200 kN |
| Max Sheet Thickness | 6.35 mm (0.25 in) |
| Punching Accuracy | 0.1 mm |
| Repeatability | 0.05 mm |
| Max Hit Rate 1mm | 910 HPM at 1 mm pitch |
| Max Hit Rate 25mm | 440 HPM at 25.4 mm pitch |
| Marking Rate | 1750 HPM |
| Feed Clearance | 80 mm (3.1 in) |
| Max Sheet Size | 3,050 x 1,550 mm (120.1 x 61.0 in) |
| Max Sheet Weight | up to 150 kg (331 lb) on the brush table, at reduced speed |
| Work Chute | 500 x 525 mm (19.7 x 20.7 in) |
| Work Clamps | 3 CNC relocatable with part pull out sensor |
| Tool Magazine | 20 stations - T-style |
| Auto Index Stations | 20 stations till 90 mm |
| Angular Positioning Accuracy | ± 0.05 degrees |
| CNC Control | Touch PL |
| Max Positioning Speed | 130 m/min. |
| Tool Change Time | 3 - 6.5 sec. |
| Power Consumption | 14.3 kW |
| Standby Power | 0.9 kW |
| Automation Options | Automatic load/unload (PA), Compact Tower (CT-P), Flexible Automation (FA-P), Bin sort, Robot pick/sort, Lubrication system |
Specifications sourced from lvdgroup.com — verified 2026-10-05
Strengths & Limitations
Strengths
- Punching, forming, tapping, bending and laser cutting in a single setup
- 4-kW fiber laser for contours and etching alongside a 200 kN single punch head
- Full-size 3050 x 1525 mm workpiece processed without repositioning
- 80 mm (3.1 in) feed clearance and forming heights up to 75 mm
- Separate 406 mm x 1524 mm chute for laser-cut parts in addition to the 500 x 525 mm work chute
Limitations
- Tool change of 3 - 6.5 sec. is slower than on the stand-alone Strippit PX-1530
- Average power consumption of 14.3 kW, against 6.7 kW for the Strippit PX-1530
- LVD's table gives no laser cutting thickness or speed for the machine
- Tower and Warehouse Automation Systems and the Extended Tool Magazine are not marked as available
Best For
Frequently Asked Questions
01
It laser cuts. The 4-kW fiber laser handles outer contours, intricate inner contours and etching, so shapes that have no matching punch tool do not need nibbling or a second machine. The punching head still does the forming, tapping and bending, with forming heights up to 75 mm.
02
LVD's table gives a nominal worksheet of 3,050 x 1,550 mm (120.1 x 61.0 in), and the feature text says a full-size workpiece of 3050 x 1525 mm is cut and punched without repositioning. Maximum punching thickness is 6.35 mm (0.25 in) and the brush table carries up to 150 kg (331 lb) at reduced speed.
03
The punching unit. The Strippit PX-L has a single head with 20 fully indexable stations, 80 mm of feed clearance and 200 kN. The Strippit V-L has a 48-station thick turret, 25 mm of feed clearance and 300 kN, with a faster tool change of 0.9 - 2.1 sec. Both carry a 4-kW laser and share the same nominal worksheet.
04
Punched parts up to 500 x 525 mm (19.7 x 20.7 in) go through the work chute. A second, larger chute of 406 mm x 1524 mm is provided for laser-cut parts and scrap. Bin sort and robot pick/sort are marked as available automation, and scrap conveyors are listed as an option.
05
The Touch-PL control (written Touch PL in the specification table), with CADMAN-PL as the programming software for both punching and laser cutting. LVD describes job setup as virtually automatic once the two are integrated. Ram cycle profiles for punching, forming and tapping are fully programmable.
More from LVD
Other CNC Punch Presses
Salvagnini S4-40
Prima Power Combi Genius
Yawei HPE-3078
TRUMPF TruPunch 2000
Amada EM 3612 ZRTe