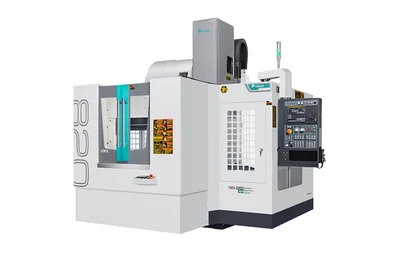
Brother SPEEDIO S700X1N

Image: brother.co.jp, Brother Industries
Key Specifications
Spindle Taper
Spindle Power
x axis travel
y axis travel
z axis travel
spindle speed
How much does the Brother SPEEDIO S700X1N cost?
Estimated price range
Our best estimate for a vertical machining centers (vmc) in this class — not a quote from Brother Industries. Configuration moves it a long way.
Overview
The Brother SPEEDIO S700X1N is the long-stroke model of the X1N vertical line: 700 mm (27.6 in) of X travel over 400 mm (15.7 in) of Y and 305 mm (12.0 in) of Z, a BT30 spindle running 10,000 rpm as standard, and a turret magazine with 14 or 21 positions.
That X stroke is the reason to pick this model. Seven hundred millimetres lets you line up several vises or a string of fixtures along the table and run them in one cycle, or machine long narrow parts such as covers, rails and manifolds without a second setup. Y and Z do not grow with it, so the machine gains length only, not depth or height.
Spindle choice deserves attention when a used or new machine is specified. The standard spindle tops out at 10,000 rpm and a 16,000 rpm spindle is listed as an option. For small end mills in aluminium the faster spindle is the one to ask for; for drilling, tapping and general milling in steel and cast iron the standard one does the job. The table gives a single power rating, 5.5 kW (7.4 hp), which rules out heavy roughing whichever spindle is fitted. BIG-PLUS holders are optional on the BT30 taper.
Axis speeds are 50 m/min (1,969 ipm) on X and Y and 48 m/min (1,890 ipm) on Z, with a chip-to-chip time of 1.4 seconds. A separate axis-speed row on the same table reads 50 × 50 × 56 m/min, which contradicts the Z figure, so treat Z rapid as unconfirmed until Brother states it for the machine in question.
Table load is 200 kg (441 lb), and on a long-X machine that limit covers everything spread along the table at once. A row of steel vises with blanks in them adds up quickly. The control is Brother's CNC-C00 and the supply is 200/220 V three-phase.
Full Specifications
| Parameter | Value |
|---|---|
| X Axis Travel | 700 mm (27.6 in) |
| Y Axis Travel | 400 mm (15.7 in) |
| Z Axis Travel | 305 mm (12.0 in) |
| Spindle Speed | 10,000 rpm (16,000 rpm optional) |
| Spindle Taper | BT30 (BIG-PLUS optional) |
| Spindle Motor Power | 5.5 kW (7.4 hp) |
| Tool Magazine | 14 or 21-position turret |
| Chip to Chip Time | 1.4 seconds |
| Rapid Traverse Xy | 50 m/min (1,969 ipm) |
| Rapid Traverse Z | 48 m/min (1,890 ipm) |
| Table Load Capacity | 200 kg (441 lb) |
| CNC Control | Brother CNC-C00 |
| Power Supply | 200/220V, 3-phase |
| Xyz | 50m/min×50m/min×56m/min |
Specifications sourced from brother.co.jp — verified 2026-03-28
Strengths & Limitations
Strengths
- 700 mm (27.6 in) of X travel for long parts or several fixtures set in a row
- Optional 16,000 rpm spindle in place of the standard 10,000 rpm for small-tool aluminium work
- Turret magazine with 14 or 21 positions and a 1.4 seconds chip-to-chip time
- X and Y rapids of 50 m/min (1,969 ipm)
- BT30 spindle taper with BIG-PLUS holders available, on Brother's CNC-C00 control
Limitations
- The standard spindle stops at 10,000 rpm; 16,000 rpm is an option, not standard
- A 5.5 kW (7.4 hp) spindle rating limits heavy cuts despite the long X stroke
- The 200 kg (441 lb) table load is shared by every fixture spread along the 700 mm (27.6 in) of X
- Z rapid is 48 m/min (1,890 ipm) in one row and 56 m/min in another, so the real figure needs confirming
Best For
Frequently Asked Questions
01
Mainly in X travel and standard spindle speed. The S700X1N has 700 mm (27.6 in) of X and a 10,000 rpm standard spindle with 16,000 rpm optional. The SPEEDIO S500X1N has 500 mm (19.7 in) of X and lists 16,000 rpm, with rapids of 50 m/min (1,969 ipm) on all axes. Y, Z, spindle power and table load are the same on both: 400 mm (15.7 in), 305 mm (12.0 in), 5.5 kW (7.4 hp) and 200 kg (441 lb).
02
No. The listed standard spindle runs to 10,000 rpm and the 16,000 rpm spindle is an option. When looking at a used S700X1N, check which spindle is fitted, because it decides whether the machine suits small-tool aluminium work or general steel drilling and tapping.
03
The Z rapid row gives 48 m/min (1,890 ipm), while a combined axis-speed row on the same table reads 50 × 50 × 56 m/min. X and Y agree at 50 m/min (1,969 ipm) in both rows. Ask Brother which Z figure is correct before using it in a cycle-time quote.
04
BT30 tools in a turret magazine with 14 or 21 positions, and BIG-PLUS dual-contact holders are listed as an option. Chip-to-chip time is 1.4 seconds, which keeps tool changes from dominating cycles on parts that use many small tools.
Videos

Lionapex Machine Tool Solutions

M+E

MTDCNC
More from Brother Industries
Other Vertical Machining Centers (VMC)
Fryer MB-14Q
YCM NTV158A
Haas VF-10/50
Kent CNC TW-32Qi

GF Machining Mikron VCE 1000 Pro