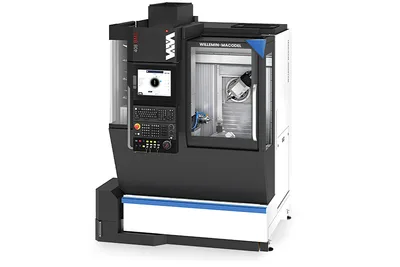
Willemin-Macodel 408MTS
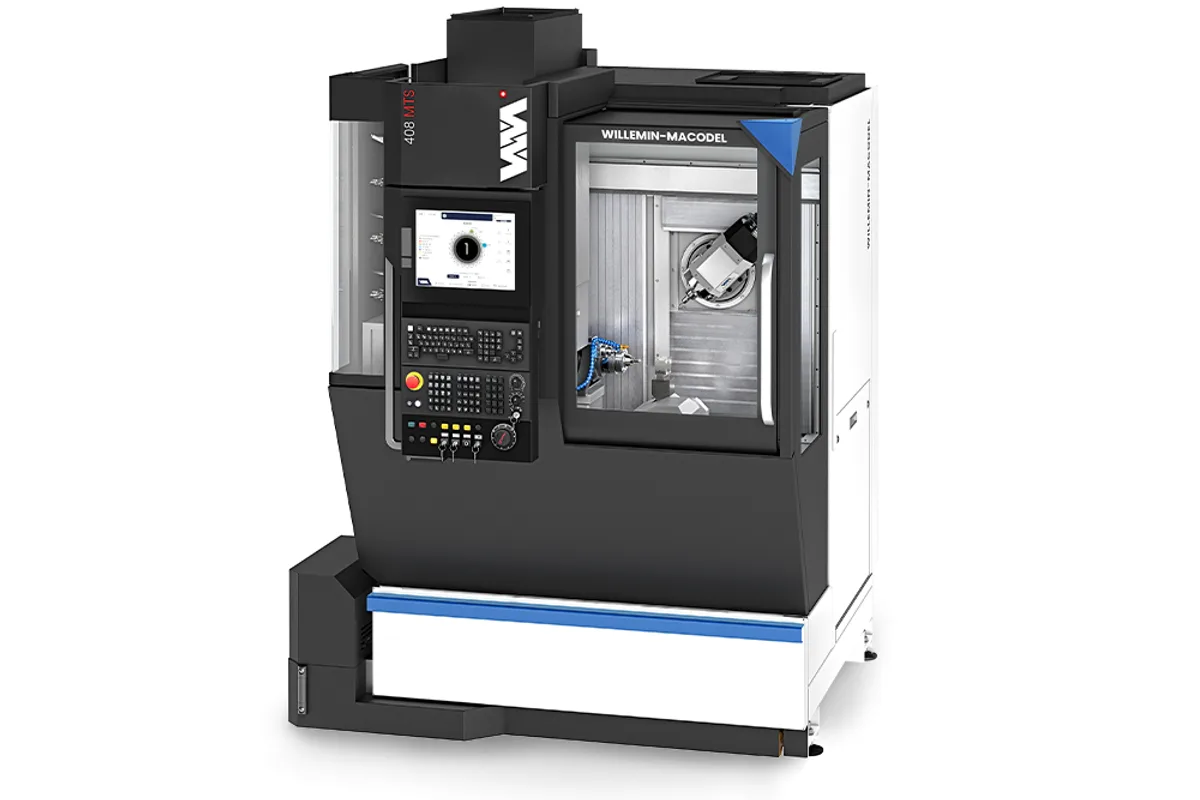
Image: willemin-macodel.com, Willemin-Macodel
Key Specifications
X Travel
Y Travel
Z Travel
Max Spindle
Spindle Taper
Tool Capacity
How much does the Willemin-Macodel 408MTS cost?
Price estimate
We do not have a price for the Willemin-Macodel 408MTS that we can stand behind, so we show no number. Configuration, options and installation move the final price a long way: a quote is the reliable figure.
Overview
The Willemin-Macodel 408MTS is the 408MT with simultaneous backworking: 8 to 9 axes, milling and turning from Ø36 mm bar, and a second spindle that finishes the cut-off side while the main spindle has already started on the next part.
Bar work begins on the A axis. It holds stock in an A4 cone, turns it at 6,000 min-1 in turning mode and positions it at 200 min-1 for milling. Above it the HSK-E40 spindle on its B axis, -15° to +100° at up to 250 min-1, brings milling cutters or fixed turning tools to the bar. Main travels are 250 mm in X, 200 mm in Y and 310 mm in Z.
Once the part is picked off, the rework unit takes over. It indexes to 0°, 90° or 180° and is served by its own linear axes, listed at 50 mm, 120 mm and 130 mm of stroke and 20 m/min. Its S3 spindle is an HSK-E25 unit at 45,000 min-1 with 8 tools. The short strokes and the small magazine mean the back operation should be the lighter half of the job: deburring, a few pockets, cross holes, engraving.
Willemin-Macodel claims productivity gains of up to 40% for the simultaneous unit and 80 on-board tools in total, 48 on S1 (72 in the bracketed size) plus those on S3. Options include a bar feeder and tool measurement and part inspection on both S1 and S3. The control is a FANUC 31i-B5 PLUS iHMI Pro.
Full Specifications
| Parameter | Value |
|---|---|
| X-Axis Travel | 250 mm (9.8 in) |
| Y-Axis Travel | 200 mm (7.9 in) |
| Z-Axis Travel | 310 mm (12.2 in) |
| Linear Axes Max Feed Speed | 40 m/min |
| Linear Axes Resolution | 0.0125 µm |
| Secondary Linear Axes Stroke X Y Z | 50 – 120 – 130 mm |
| Secondary Linear Axes Max Feed Speed | 20 m/min |
| Bar Capacity | Ø36 mm (1.4 in) |
| A Axis Interface | A4 cone |
| A Axis Speed Milling Mode | 200 min-1 |
| A Axis Speed Turning Mode | 6,000 min-1 |
| B Axis Drive | Torque motor |
| B Axis Angular Movement | -15° to +100° |
| B Axis Max Feed Speed | 250 min-1 |
| B Axis Resolution | 0.0001° |
| Rework Unit Positions | 3 positions: 0° – 90° – 180°. |
| Spindle Taper | HSK-E40 (HSK-A40/CAPTO C4) |
| Max Spindle Speed | 30,000 min-1 (42,000 min-1) |
| Spindle Lubrication | Air-oil (Grease) |
| Spindle Resolution | ±0.02° |
| Dts Dynamic Thermal Stabilization | Integrated |
| S3 Spindle Taper | HSK-E25 |
| S3 Spindle Speed Max | 45,000 min-1 |
| S3 Spindle Dts | Integrated |
| Tool Capacity | 48 (72) |
| Tool to Tool Changeover | 0.8 sec |
| Chip to Chip Change | < 3 sec |
| Tool Management | Integrated |
| Tool Breakage Detection | Masked time |
| S3 Tool Capacity | 8 |
| S3 Tool Management | Integrated |
| CNC Control | FANUC 31i-B5 PLUS iHMI Pro |
| Dimensions W X D X H | 1,685 x 1,795 x 2,305 mm (66.3 x 70.7 x 90.7 in) |
| Floor Area | 3 m² |
Specifications sourced from willemin-macodel.com — verified 2026-10-05
Strengths & Limitations
Strengths
- Turning at 6,000 min-1 and 5-axis milling from the same Ø36 mm bar
- Simultaneous backworking with an HSK-E25 S3 spindle at 45,000 min-1
- Maker-quoted productivity gains of up to 40% over sequential rework
- Rework unit indexes to 0°, 90° and 180°
- Main spindle changes tools in 0.8 sec, under 3 sec chip to chip
Limitations
- Bar capacity is Ø36 mm, below the Ø40 mm of the 408BMS
- Only 8 tools serve the S3 spindle
- Secondary axes feed at 20 m/min, half the 40 m/min of the main axes
- No spindle power or A-axis torque is published
Best For
Frequently Asked Questions
01
Both take Ø36 mm bar and turn at 6,000 min-1 on the A axis. The 408MTS adds a simultaneous backworking unit with its own linear axes, an HSK-E25 S3 spindle at 45,000 min-1 and an 8-tool magazine, so two parts are machined at once. The 408MT table lists a single spindle.
02
The main linear axes travel 250 mm in X, 200 mm in Y and 310 mm in Z at up to 40 m/min. The second set of linear axes has strokes of 50 mm, 120 mm and 130 mm and feeds at 20 m/min.
03
48 on the S1 magazine, or 72 as the bracketed size, and 8 on the S3 magazine. The maker's headline states a maximum capacity of 80 on-board tools. Turning and milling tools share the S1 magazine, and tool management is integrated on both.
04
It depends on whether the parts need turning. The 408MTS has the 6,000 min-1 turning mode and Ø36 mm bar capacity. The 408BMS is for milling only, lists the A axis at 200 min-1, and takes Ø40 mm bar. Their backworking units carry the same figures.
More from Willemin-Macodel
Other Mill-Turn / Multi-Tasking Machines
Nakamura-Tome SC-300L2

DN Solutions SMX 2100 B

Citizen Miyano BNE-51MYY
Okuma MULTUS B750
INDEX C400