Citizen Cincom M16
This model was not found in Citizen Machinery's current lineup when we checked on 2026-10-02 (lineup page). It may be a superseded or older model; the specifications below are as we last recorded them.
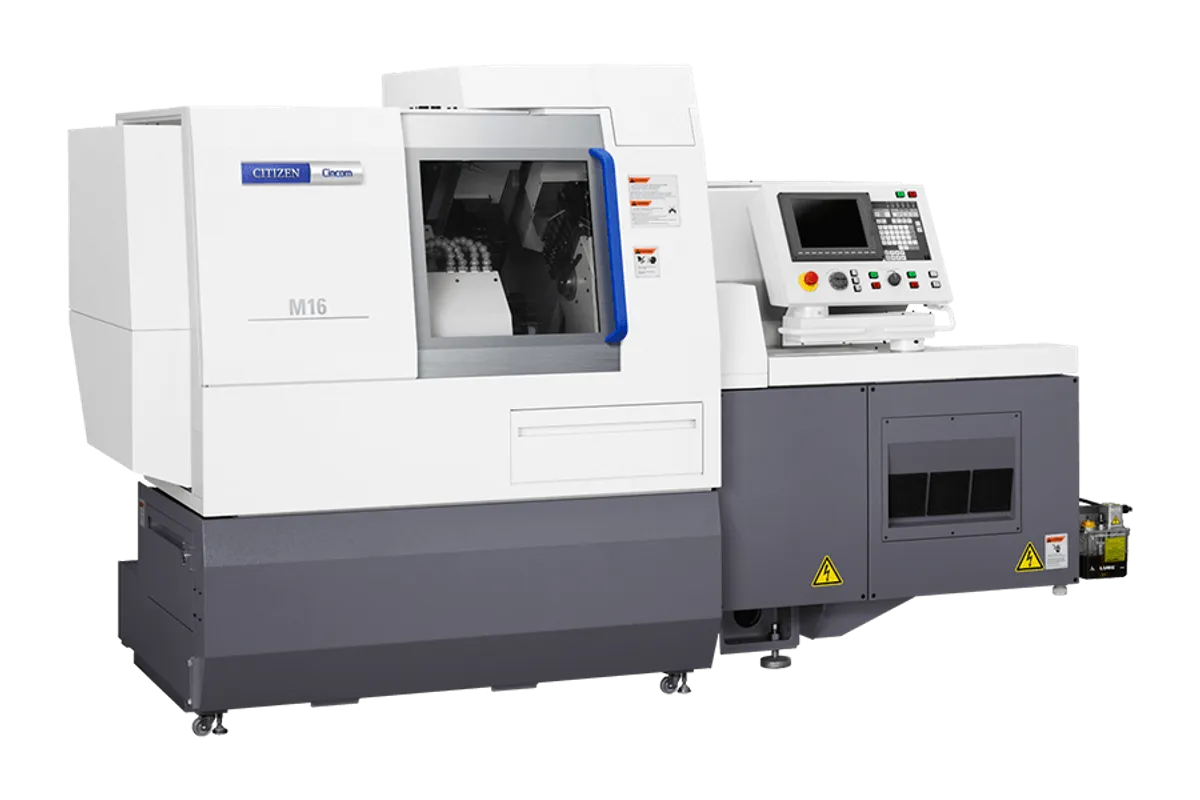
Image: cmj.citizen.co.jp, Citizen Machinery
Key Specifications
Max Spindle
Tool Capacity
Spindle Power
max machining diameter
max machining length
back spindle power
How much does the Citizen Cincom M16 cost?
Estimated price range
Our best estimate for a swiss-type lathe in this class — not a quote from Citizen Machinery. Configuration moves it a long way.
Overview
The Citizen Cincom M16 is a 16 mm (.6") Swiss-type lathe with a turret alongside its gang and back tool posts, listed with a 10,000 rpm main spindle and 200 mm (7.8") of machining length per chuck. It is not in Citizen's current lineup, and a buyer today will be looking at a used machine.
The listing for the M16 is less consistent than most. Two rows hold values that belong to other rows (a centre height given in kVA, an average power given in mm), the spindle power appears as both 2.2/3.7kW and 3.7 / 5.5 kW, and the tool capacity as both 36+α and 18. Treat those as unknown and check the nameplate and tooling of the actual machine.
The rows that do agree describe a three-post machine. Front drilling reaches 10 mm (0.394 in) with M8 taps through a 20 mm (0.787 in) spindle bore. The back spindle chuck takes 16 mm, drills 8 mm (0.315 in) and taps M6, with up to 125 mm of the workpiece protruding. Rotary tools on all tool posts run at 8,000 rpm, drilling 5 mm and tapping M5. The guide bush can be dropped as an option, LFV chip breaking is listed as standard, and the machine weighs 2,950kg with a rated power consumption of 7.9kVA.
Full Specifications
| Parameter | Value |
|---|---|
| Max Machining Diameter | 16 mm (.6") |
| Max Machining Length | 200 mm (7.8") |
| Back Spindle Power | 0.75 / 1.5 kW (1 / 2 HP) |
| Spindle Bore | 20 mm (0.787 in) |
| Number of Axes | 13 Axes |
| Rotary Tool Speed | 8,000 RPM (all tool posts) |
| Max Drilling Diameter Front | 10 mm (0.394 in) |
| Max Drilling Diameter Back | 8 mm (0.315 in) |
| Max Tapping Front | M8 |
| Max Tapping Back | M6 |
| Guide Bushing | Yes / Guide-bushless option |
| Lfv Chip Breaking | Yes (standard) |
| Machine Weight | 2,950kg |
| Center Height | 5.4kVA |
| CNC Control | PC-Based CNC System |
| Maximum Machining Diameter | 16mm Dia. |
| Maximum Machining Length | 200mm/chuck |
| Maximum Drilling Diameter for Main Spindle | 10mm Dia. |
| Maximum Front Tapping Diameter | M8 |
| Main Spindle Through Hole Diameter | 20mm Dia. |
| Max Spindle Speed | 10,000 rpm |
| Maximum Chuck Diameter of Back Spindle | 16mm Dia. |
| Maximum Protrusion Length of The Back Spindle Workpiece | 125mm |
| Maximum Drilling Diameter in Back Machining Process | 8mm Dia. |
| Maximum Tapping Diameter in Back Machining Process | M6 |
| Gang Tool Rotary Tool Maximum Drilling Diameter | 5mm Dia. |
| Gang Tool Rotary Tool Maximum Tapping Diameter | M5 |
| Spindle Speed of The Gang Rotary Tool | 8,000min-1 |
| Maximum Drilling Diameter for Turret Rotary Tool | 5mm Dia. |
| Maximum Tapping Diameter for Turret Rotary Tool | M5 |
| Maximum Drilling Diameter for Back Rotary Tool | 5mm Dia. |
| Maximum Tapping Diameter for Back Rotary Tool | M5 |
| Spindle Speed of The Back Rotary Tool | 8,000min-1 |
| Number of Tools to Be Mounted | 36+α |
| Sleeve | 19.05mm Dia. |
| X2 Axis | 16m/min |
| X3 Axis | 32m/min |
| Y1 Axis | 32m/min |
| Y2 Axis | 8m/min |
| Y3 Axis | 32m/min |
| Z1 Axis | 32m/min |
| Z2 Axis | 32m/min |
| Z3 Axis | 32m/min |
| For Back Spindle Drive | 0.75/1.5kW |
| For Tool Spindle Drive | 0.69kW |
| For Back Tool Spindle Drive | 0.75kW |
| For Cutting Coolant Oil | 0.4kW |
| Rated Power Consumption | 7.9kVA |
| Load Operation Average Power | 1,150mm |
| Tool Size Turning Tool | 10mm Sq. |
| Tool Size Sleeve | 19.05mm Dia. |
| Rapid Feed Rate X1 Axis | 32m/min |
| Rapid Feed Rate X2 Axis | 16m/min |
| Rapid Feed Rate X3 Axis | 32m/min |
| Rapid Feed Rate Y1 Axis | 32m/min |
| Rapid Feed Rate Y2 Axis | 8m/min |
| Rapid Feed Rate Y3 Axis | 32m/min |
| Rapid Feed Rate Z1 Axis | 32m/min |
| Rapid Feed Rate Z2 Axis | 32m/min |
| Rapid Feed Rate Z3 Axis | 32m/min |
| Motors for Spindle Drive | 2.2/3.7kW |
| Motors for Back Spindle Drive | 0.75/1.5kW |
| Motors for Tool Spindle Drive | 0.69kW |
| Motors for Back Tool Spindle Drive | 0.75kW |
| Motors for Cutting Coolant Oil | 0.4kW |
| Sub Spindle Speed | 6,000 rpm |
| Tool Capacity | 18 Tools |
| Turret Stations | 10-Station Turret |
| Spindle Motor Power | 3.7 / 5.5 kW (5 hp) |
Specifications sourced from marucit.com — verified 2026-09-24
Strengths & Limitations
Strengths
- Turret plus gang and back tool posts, with rotary tools on each
- Up to 125 mm of workpiece protrusion from the back spindle
- LFV chip breaking listed as standard
- Guide-bushless operation available as an option
Limitations
- Not in Citizen's current lineup, and several listed rows conflict
- Main spindle listed at 10,000 rpm, below the 12,000 rpm of the current Cincom M16-VIII
- Rotary tools limited to 5 mm drilling and M5 tapping
Best For
Frequently Asked Questions
01
No, it is not in Citizen's current lineup. The current machine is the Cincom M16-VIII, which lists 12,000 rpm on the main spindle and a weight of 2,950 kg, against the 10,000 rpm listed for the M16.
02
The spindle power, listed as both 2.2/3.7kW and 3.7 / 5.5 kW, and the tool capacity, listed as both 36+α and 18. The centre height and average power rows also hold each other's values. Confirm all of these from the machine's nameplate and documentation.
03
The back spindle chuck takes 16 mm bar and allows up to 125 mm of workpiece protrusion. It drills up to 8 mm (0.315 in) and taps M6. Back rotary tools drill 5 mm and tap M5 at 8,000 rpm.
04
Most axes rapid at 32 m/min: X1, X3, Y1, Y3, Z1, Z2 and Z3. The X2 axis is listed at 16 m/min and the Y2 axis at 8 m/min, half and a quarter of that rate, which matters on jobs where those axes do much of the positioning.
Videos

Citizen Machinery UK

Automatics & Machinery

Automatics & Machinery

CNC HELP
Community Discussions
Links to community discussions. Summaries are editorial — visit the original thread for full context.
More from Citizen Machinery



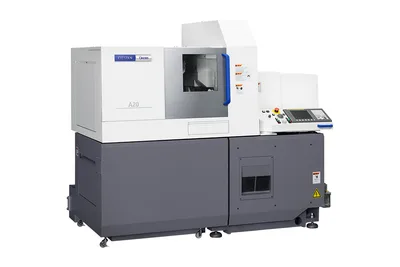
Other Swiss-Type Lathes
Tsugami SS207-II
Star SB-38
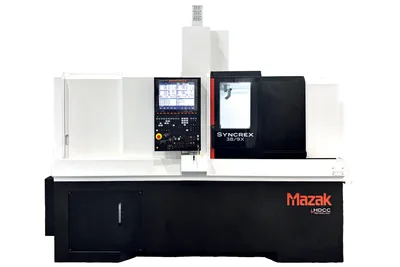
Mazak SYNCREX 20/8
Tsugami BW127-II
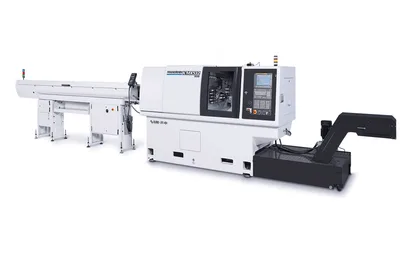
Tajmac-ZPS MANURHIN K'MX 532 TREND