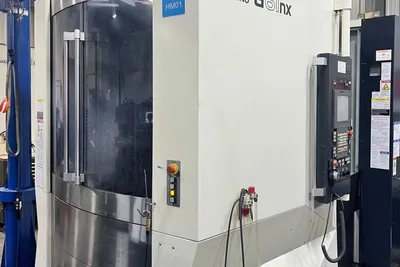
Kitamura Mycenter-HX500iG #40
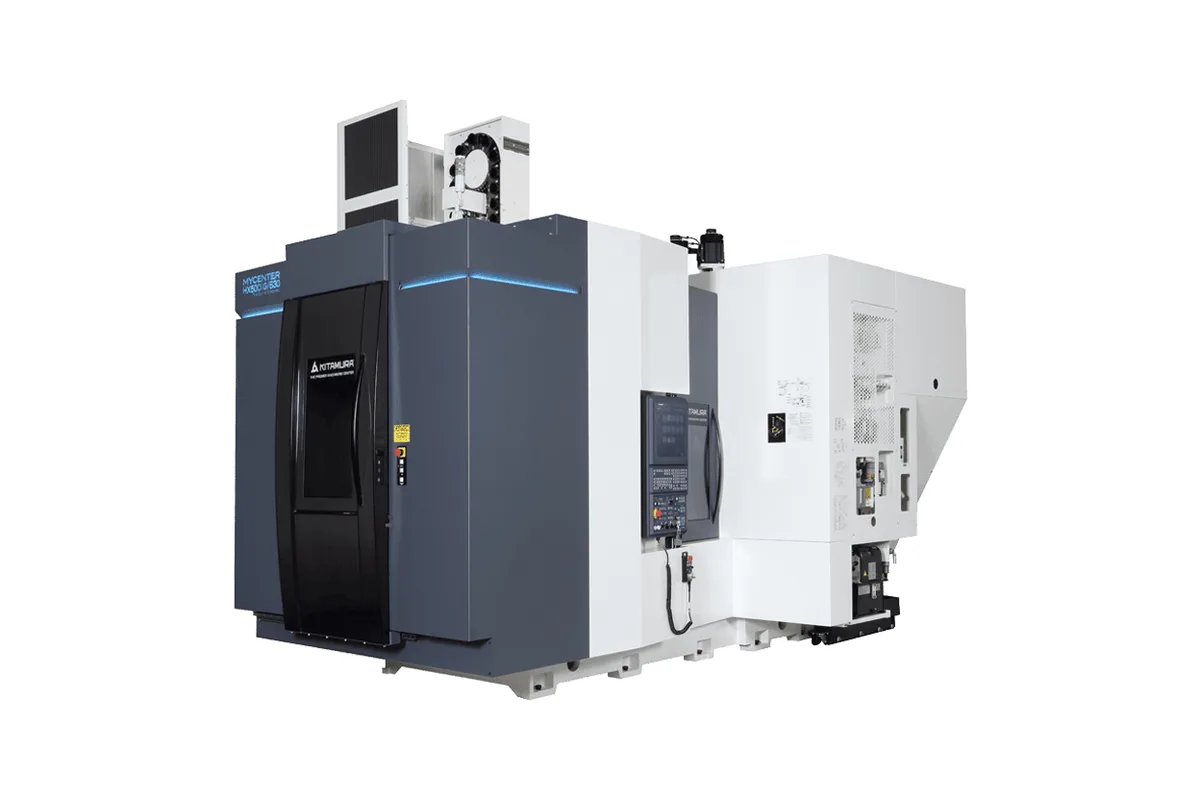
Image: kitamura-machinery.com, Kitamura Machinery
Key Specifications
X Travel
Y Travel
Z Travel
Max Spindle
Spindle Taper
Tool Capacity
How much does the Kitamura Mycenter-HX500iG #40 cost?
Estimated price range
Our best estimate for a horizontal machining centers (hmc) in this class — not a quote from Kitamura Machinery. Configuration moves it a long way.
Overview
Kitamura's Mycenter-HX500iG #40 pairs a 500 x 500 mm (19.7 x 19.7 in) pallet with a No. 40 taper spindle that is gear driven through four steps and runs from 20 to 20,000 rpm. That speed range is what sets this build apart. A 40-taper spindle fast enough for small tools normally has little to offer at the bottom of its range; here the gear steps are the reason one spindle can turn a large drill slowly and still finish with a small end mill at 20,000 rpm.
Travels are 870 mm (34.3 in) in X, 800 mm (31.5 in) in Y and 930 mm (36.6 in) in Z. The work envelope accepts a part or fixture stack up to 800 mm (31.5 in) in diameter and 1,100 mm (43.3 in) tall, well beyond the 500 mm footprint of the pallet itself, so tall tombstones and overhanging fixtures are part of the plan. No workpiece weight limit appears in the table. Get that figure confirmed before quoting a heavy casting or a fully loaded tombstone.
Between cuts the figures are 1.3 sec tool-to-tool, 3.8 sec chip-to-chip, 60 m/min (2,362 ipm) rapids and a B axis that turns at 120 rpm (43,200 deg/min). The standard magazine holds 50 tools, with 62, 100, 150, 200 and 300 tool magazines as options. The Mycenter-HX500iG #50 shares the pallet and travels but carries a No. 50 taper spindle at 35 to 12,000 rpm with 54 HP and a 62 tool magazine, which is the build for larger cutters.
Positioning accuracy is ±0.001 mm (±0.000039 in) over the full stroke, with ±0.0005 mm (±0.00002 in) repeatability. HSK-A63 is the optional taper. The control is the Arumatik-Mi CNC, and the machine draws 55 kVA at 200 V AC, three-phase.
Full Specifications
| Parameter | Value |
|---|---|
| Pallet Size | 500 x 500 mm (19.7 x 19.7 in) |
| X-Axis Travel | 870 mm (34.3 in) |
| Y-Axis Travel | 800 mm (31.5 in) |
| Z-Axis Travel | 930 mm (36.6 in) |
| Max Workpiece Diameter | 800 mm (31.5 in) |
| Max Workpiece Height | 1,100 mm (43.3 in) |
| Max Spindle Speed | 20 - 20,000 rpm 4-Step Gear Driven |
| Spindle Taper | NST No. 40 (HSK-A63 optional) |
| Spindle Drive | 4-step gear driven |
| Tool Capacity | 50 tools (62, 100, 150, 200, 300 Tools optional) |
| Tool Change Time | 1.3 sec (T-T) / 3.8 sec (C-C) |
| Rapid Traverse Rate | 60 m/min (2,362 ipm) |
| Positioning Accuracy | ±0.001mm (±0.000039")/Full Stroke |
| Repeatability | ±0.0005mm (±0.00002") |
| Table Size | 500 × 500 mm (19.7 × 19.7 in) |
| Electrical | 55KVA, 200v AC, 3 Phase |
| CNC Control | Arumatik-Mi CNC |
| Tool to Tool Time | 1.3 sec |
| Chip to Chip Time | 3.8 sec |
| Rotary Indexing Speed B | 120 rpm (43,200deg./min) |
| Power Supply | 55 kVA, 200 V AC, 3-phase |
Specifications sourced from kitamura-machinery.com — verified 2026-10-03
Strengths & Limitations
Strengths
- Four-step gear-driven No. 40 spindle covering 20 to 20,000 rpm, so slow heavy tools and fast small tools run on one spindle
- Work envelope of 800 mm (31.5 in) diameter by 1,100 mm (43.3 in) height above a 500 x 500 mm (19.7 x 19.7 in) pallet
- Tool changes of 1.3 sec tool-to-tool and 3.8 sec chip-to-chip, backed by 60 m/min (2,362 ipm) rapids
- ±0.001 mm (±0.000039 in) positioning accuracy over the full stroke and ±0.0005 mm (±0.00002 in) repeatability
- B axis rotates at 120 rpm (43,200 deg/min), which keeps face-to-face indexing short
Limitations
- No spindle power or torque is listed for this build, whereas the Mycenter-HX500iG #50 is listed at 54 HP
- The table gives no maximum workpiece weight, so pallet load has to be confirmed with Kitamura
- The 62, 100, 150, 200 and 300 tool magazines are options; the standard machine carries 50 tools
- HSK-A63 is an option, and the electrical requirement is 55 kVA at 200 V AC, three-phase
Best For
Frequently Asked Questions
01
The spindle and the magazine. The Mycenter-HX500iG #40 has a No. 40 taper spindle running from 20 to 20,000 rpm and a 50 tool standard magazine. The Mycenter-HX500iG #50 has a No. 50 taper spindle at 35 to 12,000 rpm with 54 HP and a 62 tool magazine. Both use the 500 x 500 mm (19.7 x 19.7 in) pallet with 870 mm (34.3 in), 800 mm (31.5 in) and 930 mm (36.6 in) of travel.
02
Up to 800 mm (31.5 in) in diameter and 1,100 mm (43.3 in) in height, on a 500 x 500 mm (19.7 x 19.7 in) pallet. The table does not state a maximum workpiece weight, so confirm the pallet load with Kitamura if the part and fixture together are heavy.
03
The spindle is listed as four-step gear driven with a range of 20 to 20,000 rpm. Gear steps trade speed for torque, so the lower steps serve large drills, taps and face mills while the top step serves small cutters. Kitamura's table for this build does not give power or torque figures, so ask for the output in each gear step.
04
50 tools as standard. Magazines of 62, 100, 150, 200 and 300 tools are optional. The changer runs 1.3 sec tool-to-tool and 3.8 sec chip-to-chip. HSK-A63 can be ordered in place of the standard NST No. 40 taper.
05
When the part or fixture outgrows a 500 mm pallet. The Mycenter-HX630G #40 has the same 20 to 20,000 rpm four-step gear-driven spindle, listed at 30 HP, on a 630 x 630 mm (24.8 x 24.8 in) pallet with travels of 1,100 mm (43.3 in), 920 mm (36.2 in) and 1,050 mm (41.3 in).
06
55 kVA at 200 V AC, three-phase. The control is Kitamura's Arumatik-Mi CNC. Rapid traverse is 60 m/min (2,362 ipm), so the supply has to support fast axis moves as well as the spindle.
Videos

KitamuraMachinery2

MÁY CƠ KHÍ - Á CHÂU
More from Kitamura Machinery



Other Horizontal Machining Centers (HMC)
DMG Mori DMF 180
Fryer HR-14