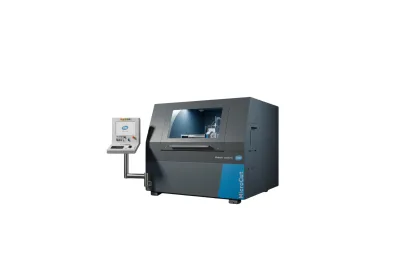
KMT Streamline PRO CNC Waterjet System
Key Specifications
Accuracy
table sizes
pump pressure
pump power
drive technology
cutting head
How much does the KMT Streamline PRO CNC Waterjet System cost?
Estimated price range
Our best estimate for a cnc waterjet cutting in this class — not a quote from KMT Waterjet. Configuration moves it a long way.
Overview
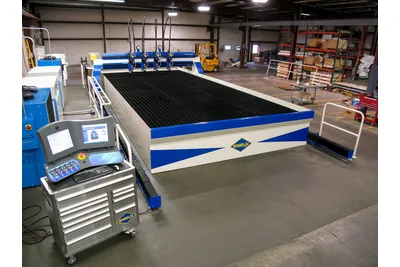
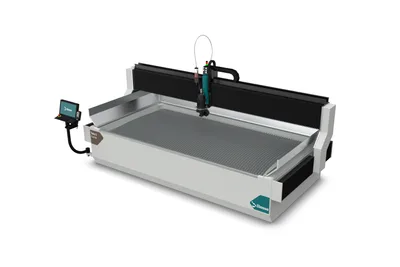
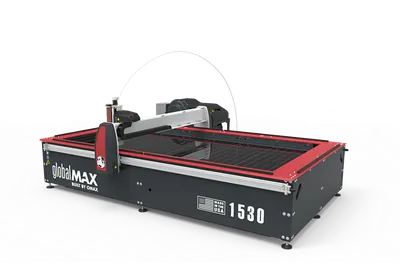
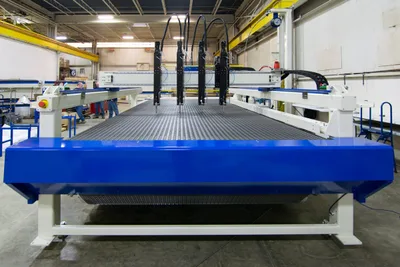
The KMT Streamline PRO CNC Waterjet System is listed as a complete abrasive cutting system, not a pump on its own: tables from 4x4 ft to 13x6 ft, pump pressure of 60,000 to 90,000 PSI and pump power from 30 HP to 125 HP. No page for a system under this name was found on KMT Waterjet's own site, so everything below rests on the listed figures, which are unverified. Ask the seller for a specification sheet for the exact configuration on offer.
That matters more than usual here because the table describes a family. Table size, pressure and horsepower are all given as ranges, and nothing says which pump goes with which table. A 4x4 ft machine and a 13x6 ft machine are different purchases, and so are a 30 HP pump and a 125 HP one.
The fixed figures are few. Positioning accuracy is listed at ±0.05 mm. Maximum thickness is 150 mm in steel, a limit that in practice depends on where in the pressure and power range the pump sits. Abrasive flow is adjustable from 0.1 to 1.2 kg/min of garnet, and a function the table calls Shift Cut is described as optimizing abrasive consumption. Garnet is the main consumable in abrasive cutting, so that range and that function bear directly on how much of it each part uses.
On the software side the control row gives IGEMS CAD/CAM as standard. The cutting head is listed as a KMT AUTOLINE or STREAMLINE head, without saying which is fitted by default. The drive row calls the pump a KMT direct-drive intensifier and describes it as low maintenance, but no service interval is listed to back that up.
Full Specifications
| Parameter | Value |
|---|---|
| Table Sizes | 4x4 ft to 13x6 ft (various configurations) |
| Pump Pressure | 60,000 to 90,000 PSI |
| Pump Power | 30 HP to 125 HP direct-drive intensifier |
| Drive Technology | KMT direct-drive intensifier (low maintenance) |
| Positioning Accuracy | ±0.05 mm |
| Cutting Head | KMT AUTOLINE or STREAMLINE head |
| CNC Control | IGEMS CAD/CAM (standard) |
| Maximum Thickness | 150 mm steel |
| Abrasive Flow | 0.1 – 1.2 kg/min garnet |
| Operating Cost Reduction | Shift Cut optimizes abrasive consumption |
Specifications compiled from manufacturer literature and industry references. Not independently verified against a published spec sheet — confirm with the manufacturer or an authorised dealer before making a purchasing decision.
Strengths & Limitations
Strengths
- Table sizes from 4x4 ft to 13x6 ft, so the system is listed for both small and large sheet formats
- Pump pressure of 60,000 to 90,000 PSI with 30 HP to 125 HP of pump power, depending on configuration
- Listed positioning accuracy of ±0.05 mm
- IGEMS CAD/CAM is listed as standard, not as an option
- Abrasive flow adjustable from 0.1 to 1.2 kg/min of garnet, with Shift Cut listed for optimizing abrasive consumption
Limitations
- The listed figures are unverified, so the configuration on offer has to be confirmed in writing
- Table size, pressure and power are given only as ranges, with nothing to say which pump is paired with which table
- Maximum thickness is listed as 150 mm in steel, with no figure for any other material
- The table gives no cutting speeds, axis travels, rapid rates or machine weight
Best For
Frequently Asked Questions
01
The table gives 4x4 ft to 13x6 ft in various configurations. It does not list the intermediate sizes or the axis travels for any of them, so the cutting envelope of a particular machine has to come from its own specification sheet.
02
The listing gives a pump pressure of 60,000 to 90,000 PSI and pump power of 30 HP to 125 HP, described as a KMT direct-drive intensifier. Which pressure and which horsepower a given machine has is not stated, and that choice decides cutting speed and thickness more than any other row.
03
Maximum thickness is listed as 150 mm in steel. No figures are given for stone, glass, aluminium or composites, and no cutting speed is listed at any thickness, so ask for test cuts in your own material before relying on the 150 mm figure.
04
The control row lists IGEMS CAD/CAM as standard. The cutting head is listed as a KMT AUTOLINE or STREAMLINE head, without saying which one is the default. The table also names Shift Cut as a function that optimizes abrasive consumption.
05
Abrasive flow is listed as 0.1 to 1.2 kg/min of garnet, a twelvefold range that covers fine orifices and heavy cuts alike. The table also lists Shift Cut as a function that optimizes abrasive consumption, without a figure for the saving. Actual use depends on the nozzle fitted and the cut being made.