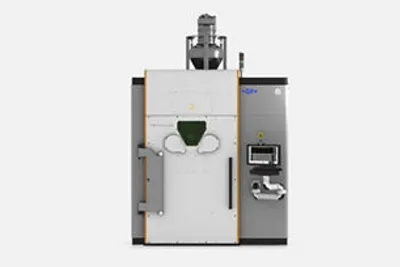
SLM Solutions SLM 500 Quad
Key Specifications
build volume
laser count
laser power
build rate
layer thickness
supported materials
How much does the SLM Solutions SLM 500 Quad cost?
Estimated price range
Our best estimate for a metal additive manufacturing in this class — not a quote from SLM Solutions. Configuration moves it a long way.
Overview
The SLM 500 Quad is a four-laser powder bed machine for production work: 4 x 700 W fiber lasers over a 500 x 280 x 365 mm (19.7 x 11 x 14.4 in) build volume, with a build rate of up to 171 cc/hr that SLM Solutions qualifies as quad-laser and material dependent.
Two rows in the table are about keeping the lasers busy. The recoater is bi-directional and works simultaneously with laser scanning, so powder is spread on both strokes instead of the blade returning empty. Powder handling is closed-loop, with automated sieving and recirculation, which keeps unused powder inside the system between builds.
The supported material list is long: Ti-6Al-4V, Inconel 718, Inconel 625, AlSi10Mg, Scalmalloy, 316L SS, 17-4PH, CoCr, maraging steel and copper. The atmosphere is inert gas, argon or nitrogen depending on the material, so a shop that runs alloys from both groups should plan for both supplies. Layer thickness runs from 20 - 90 µm (0.0008 - 0.0035 in).
Process monitoring is Integrated Process Monitoring (IPM), covering optical tomography, melt pool and a smoke sensor. Build preparation goes through the Nikon SLM Solutions Build Processor with Materialise Magics integration. For regulated parts, ask which monitoring channels are recorded per layer and how the records are exported; the table names the sensors but not the reporting.
On site the machine weighs approx. 4,200 kg (9,259 lb) and needs a 3-phase, 400 V, 63 A supply. The SLM 800 uses the same 4 × 700 W laser set and weighs approx. 8,500 kg, roughly double, so the 500 Quad is the lighter installation of the two.
Full Specifications
| Parameter | Value |
|---|---|
| Build Volume | 500 x 280 x 365 mm (19.7 x 11 x 14.4 in) |
| Laser Count | 4 |
| Laser Power | 4 x 700 W fiber lasers |
| Build Rate | Up to 171 cc/hr (quad-laser, material dependent) |
| Layer Thickness | 20 - 90 um (0.0008 - 0.0035 in) |
| Supported Materials | Ti-6Al-4V, Inconel 718, Inconel 625, AlSi10Mg, Scalmalloy, 316L SS, 17-4PH, CoCr, maraging steel, copper |
| Recoater Type | Bi-directional recoater (simultaneous with laser scanning) |
| Atmosphere | Inert gas (argon or nitrogen, material dependent) |
| Process Monitoring | Integrated Process Monitoring (IPM) — optical tomography, melt pool, smoke sensor |
| Powder Handling | Closed-loop automated sieving and recirculation |
| Software | Nikon SLM Solutions Build Processor + Materialise Magics integration |
| Machine Weight | Approx. 4,200 kg (9,259 lb) |
| Power Requirements | 3-phase, 400V, 63A |
Specifications sourced from nikon-slm-solutions.com — verified 2026-03-28
Strengths & Limitations
Strengths
- Four 700 W fiber lasers over a 500 x 280 x 365 mm (19.7 x 11 x 14.4 in) build volume
- Bi-directional recoater that works simultaneously with laser scanning
- Closed-loop powder handling with automated sieving and recirculation
- Integrated Process Monitoring (IPM) with optical tomography, melt pool and smoke sensor channels
- Wide supported material range, from Ti-6Al-4V and Inconel 718 to Scalmalloy, 17-4PH and copper
- Build Processor software with Materialise Magics integration
Limitations
- The build rate of up to 171 cc/hr is a quad-laser, material-dependent maximum, not a figure for every alloy
- 365 mm (14.4 in) of build height limits tall parts
- Atmosphere is argon or nitrogen depending on material, so a mixed-alloy shop needs both gas supplies
- Needs a 3-phase, 400 V, 63 A supply and a floor that takes approx. 4,200 kg (9,259 lb)
Best For
Frequently Asked Questions
01
500 x 280 x 365 mm (19.7 x 11 x 14.4 in). The plate is rectangular, so long parts lie along the 500 mm axis and the 365 mm height is the limit for anything built upright. Leave margin for supports and for cutting the part off the plate when a job is close to that height.
02
Up to 171 cc/hr, a figure SLM Solutions gives for quad-laser operation and describes as material dependent. Two things in the table support it: 4 x 700 W fiber lasers, and a bi-directional recoater that spreads powder simultaneously with laser scanning. Layer thickness, which runs from 20 - 90 µm (0.0008 - 0.0035 in), moves the rate up or down.
03
The supported materials are Ti-6Al-4V, Inconel 718, Inconel 625, AlSi10Mg, Scalmalloy, 316L SS, 17-4PH, CoCr, maraging steel and copper. The build chamber runs under inert gas, argon or nitrogen, and which of the two is used depends on the material.
04
Integrated Process Monitoring (IPM), which SLM Solutions describes as optical tomography, melt pool monitoring and a smoke sensor. The table does not describe how the data is stored or reported, so anyone who needs per-build records for qualification should ask for the export formats.
05
A 3-phase, 400 V, 63 A electrical supply, inert gas (argon or nitrogen, depending on the material) and a floor rated for approx. 4,200 kg (9,259 lb). The table does not give a footprint or gas consumption, so get the installation drawing before planning the cell.
Videos

Nikon SLM Solutions

Nikon SLM Solutions

Nikon SLM Solutions

Manolis Marinakis
More from SLM Solutions
Other Metal Additive Manufacturing
Colibrium Additive Concept M2 Series 5
GE Additive Arcam A2XX
Renishaw RenAM 500E
3D Systems DMP Factory 500
GE Additive Arcam EBM Q10plus