Mazak INTEGREX i-350H AG
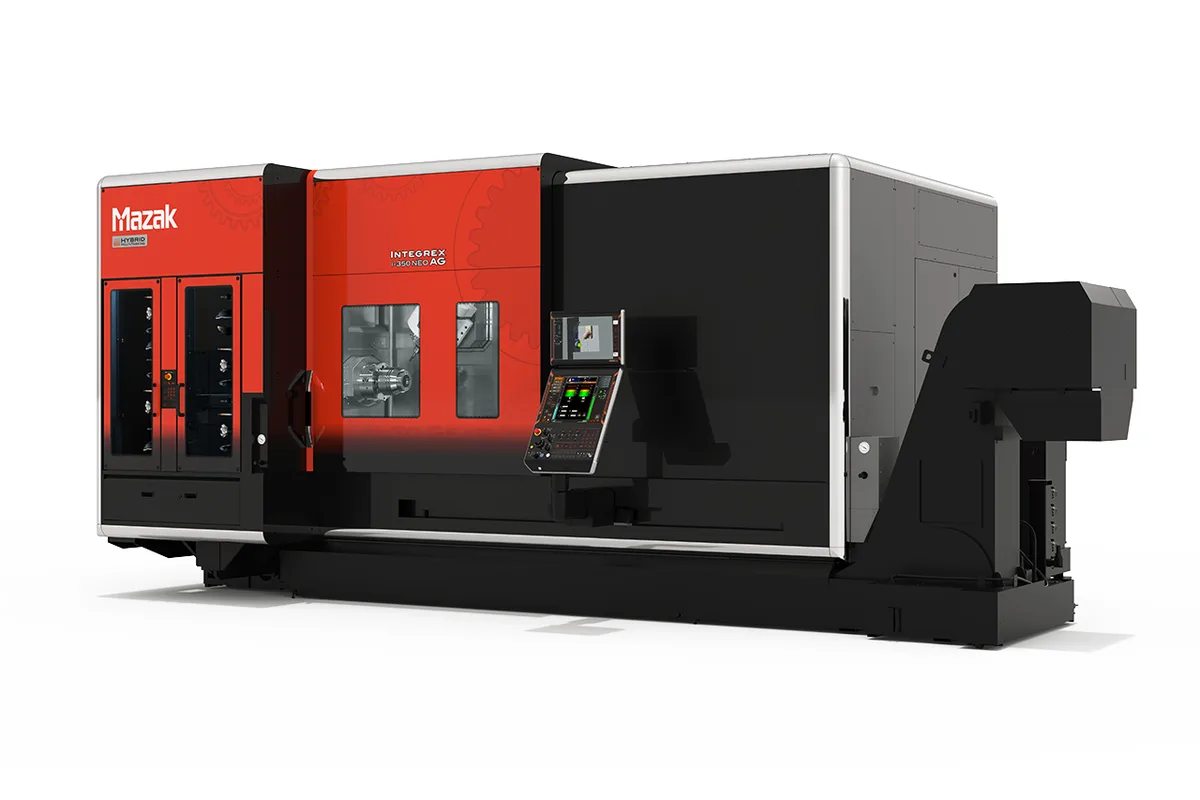
Image: mazak.com, Yamazaki Mazak
Key Specifications
X Travel
Y Travel
Z Travel
Max Spindle
Spindle Taper
Tool Capacity
How much does the Mazak INTEGREX i-350H AG cost?
Estimated price range
Our best estimate for a mill-turn / multi-tasking machine in this class — not a quote from Yamazaki Mazak. Configuration moves it a long way.
Overview
The Mazak INTEGREX i-350H AG is a 10 in chuck machine in Mazak's INTEGREX AG series, the multi-tasking line that integrates gear skiving, hobbing and endmilling with turning, milling and 5-axis machining. Its own table reads like any 10 in chuck mill-turn, with Ø26 in (660 mm) of turning diameter, 40 in (1,016 mm) of turning length, a 4,000 rpm turning spindle and a 12,000 rpm HSK-A63 milling spindle.
The three gear methods answer different batch sizes. Endmilling cuts the teeth one by one with a commercially available end mill through Mazak's Smooth Gear Milling software, which suits small lots because no dedicated cutter or jig has to be prepared. Hobbing and skiving use specialised tools and are aimed at volume. Mazak states that for gear skiving the rotational synchronisation between the turning spindle and the milling spindle is held even at the maximum speed of each spindle, and that skiving can be done with a small-diameter cutter on a small-diameter workpiece or with a carbide cutter.
Measurement is part of the same setup. Mazak lists pitch measurement with a touch probe after machining, giving single pitch error, cumulative pitch error and tooth space runout, and gear profile and gear lead measurement with a scanning probe, the latter marked with an asterisk. After skiving or hobbing the machine can identify the centre angle of a tooth groove and use that phase for keyway machining, drilling and deburring.
Both spindles are rated 22 kW (30 HP) continuous. The turning spindle gives 30 kW (40 HP) at 40% ED and the milling spindle 124 Nm (91 ft-lb) at 40% ED. Travels are 27 in (686 mm), 12 in (305 mm) and 42 in (1,067 mm) in X, Y and Z, the magazine holds 38 tools, and the machine weighs 29,652 lb (13,450 kg).
Full Specifications
| Parameter | Value |
|---|---|
| Bed Length Type | 1000U |
| Max Turning Diameter | Ø26 in (660 mm) |
| Max Turning Length | 40 in (1,016 mm) |
| Chuck Size | 10 in |
| Max Spindle Speed | 4,000 rpm |
| Spindle Power Intermittent | 30 kW (40 HP) (40% ED) |
| Spindle Motor Power | 22 kW (30 HP) continuous |
| Milling Spindle Speed | 12,000 rpm |
| Milling Spindle Torque Intermittent | 124 Nm (91 ft-lb) (40% ED) |
| Milling Spindle Torque | 91.3 Nm (67 ft-lb) continuous |
| Milling Spindle Power Intermittent | 24 kW (32 HP) (40% ED) |
| Milling Spindle Power | 22 kW (30 HP) continuous |
| B Axis Indexing Increment | 0.0001° |
| Spindle Taper | HSK-A63 |
| Tool Capacity | 38 tools |
| Max Tool Diameter (full magazine) | Ø4 in (102 mm) |
| Max Tool Diameter (adjacent pockets empty) | Ø5 in (127 mm) |
| Max Tool Length | 16 in (406 mm) |
| Max Tool Weight | 26 lb (12 kg) |
| X-Axis Travel | 27 in (686 mm) |
| Y-Axis Travel | 12 in (305 mm) |
| Z-Axis Travel | 42 in (1,067 mm) |
| B Axis Range | -30° - +210° |
| Rapid Traverse X | 1,969 ipm (50 m/min) |
| Rapid Traverse Y | 1,575 ipm (40 m/min) |
| Rapid Traverse Z | 1,969 ipm (50 m/min) |
| Tailstock Taper | MT No.5 |
| Tailstock Thrust | 2,248 lb (1,020 kg) |
| Floor Space Required | 164 in (4,166 mm) × 106 in (2,692 mm) (W × L) |
| Machine Height | 107 in (2,718 mm) |
| Machine Weight | 29,652 lb (13,450 kg) |
Specifications sourced from mazak.com — verified 2026-10-02
Strengths & Limitations
Strengths
- The INTEGREX AG series integrates three gear machining methods, gear skiving, hobbing and endmilling, with turning, milling and 5-axis machining
- Gear endmilling with commercially available end mills through Smooth Gear Milling, with tooth profile and tooth lead correction functions
- Pitch measurement with a touch probe after machining, reporting single pitch error, cumulative pitch error and tooth space runout
- Gear tooth phase can be identified after skiving or hobbing and used for keyway machining, drilling and deburring
- 22 kW (30 HP) continuous at both the 4,000 rpm turning spindle and the 12,000 rpm milling spindle
- 38-tool magazine with an HSK-A63 taper
Limitations
- Jet stream chuck coolant, which Mazak says reduces chip bite on the gear surface in internal skiving, is optional
- Gear profile and gear lead measurement with the scanning probe carries an asterisk on Mazak's list, so confirm it is included
- Cutting tools are capped at Ø4 in (102 mm) with a full magazine and 26 lb (12 kg), which bounds the hob and skiving cutter sizes that can be loaded
- Maximum turning diameter of Ø26 in (660 mm) and turning length of 40 in (1,016 mm) set the upper limit on gear blank size
Best For
Frequently Asked Questions
01
It marks the machine as part of Mazak's INTEGREX AG series, which Mazak describes as performing turning, milling, 5-axis machining and gear machining. Three gear methods are integrated in the one machine: gear skiving, hobbing and endmilling. Gear measurement is listed as part of the same process.
02
Endmilling. Mazak notes that for high-mix, low-volume parts, specialised tools such as hob cutters take a lot of time just to prepare along with their jigs. With the Smooth Gear Milling software the teeth are cut one at a time with a standard end mill, and tooth profile and tooth lead correction functions modify the machined teeth.
03
Yes. Pitch measurement is done with a touch probe after machining and gives single pitch error, cumulative pitch error, tooth space runout and the pitch circle centre. Gear profile and gear lead are measured with a scanning probe; Mazak marks that function with an asterisk, so check that it is on the quotation.
04
Mazak's series description cites ISO Class 7 machining accuracy in connection with Smooth Gear Hobbing, its programming support software for hobbing. That software has a hob shift function, which moves the cutting point along the hob on each pass to extend the interval between resharpening, and a tooth lead modification function.
05
A 10 in chuck, Ø26 in (660 mm) maximum turning diameter and 40 in (1,016 mm) maximum turning length. The turning spindle runs to 4,000 rpm and the milling spindle to 12,000 rpm, each rated 22 kW (30 HP) continuous. The footprint is 164 in (4,166 mm) × 106 in (2,692 mm) (W × L) and the weight 29,652 lb (13,450 kg).
06
An optional feature of the INTEGREX AG series. Mazak says it reduces chip bite into the gear surface during internal gear skiving and extends tool life. The nozzle can be adjusted to rotate the scattering angle between 40° and 95°.
Videos

Yamazaki Mazak Corporation [English]

John Hart

IndustryArena GmbH
Community Discussions
Pricing and buying discussion
Links to community discussions. Summaries are editorial — visit the original thread for full context.
More from Yamazaki Mazak
Other Mill-Turn / Multi-Tasking Machines
Huron MTX 200
Willemin-Macodel 808MT2

Hurco TM8MYi

DN Solutions SMX 2100
