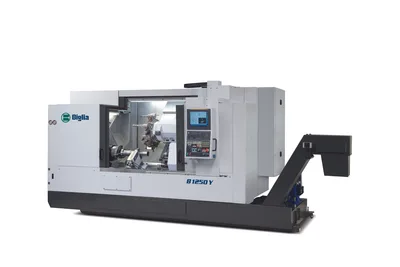
Hardinge Talent 10/78
This model was not found in Hardinge's current lineup when we checked on 2026-10-03 . It may be a superseded or older model; the specifications below are as we last recorded them.
Key Specifications
X Travel
Z Travel
Max Spindle
Spindle Power
chuck size
maximum bar capacity
How much does the Hardinge Talent 10/78 cost?
Estimated price range
Our best estimate for a cnc lathes / turning center in this class — not a quote from Hardinge. Configuration moves it a long way.
Overview
The Hardinge Talent 10/78 puts a large through-hole on a gang-tool machine: 78 mm (3.07 in) of spindle bore and bar capacity, a 10 in (254 mm) chuck size, and tools carried on a flat slide instead of a turret. The listed envelope is 300 mm (11.81 in) in maximum turning diameter and 500 mm (19.69 in) in maximum turning length.
The combination is specific. A 78 mm bore passes large bar and tube, and the spindle has the torque to cut it: 15 kW (20 hp) and a maximum of 250 Nm (184 ft-lb), at up to 4,000 RPM. Tooling on a flat slide then favours parts that need only a few tools, because each one has to clear a large workpiece as the slide moves from tool to tool. Short rings, bushings, flanges and couplings cut from big bar fit that pattern; parts with many operations do not.
X travel is 200 mm (7.87 in) and Z travel 500 mm (19.69 in). With gang tooling the X stroke is shared between the tools on the slide, so 200 mm does not go as far as it would on a turret machine. Live tooling is listed as optional, and workholding as collet-ready with a 10 in hydraulic chuck.
Rapids are 20 m/min (787 ipm) in X and 24 m/min (945 ipm) in Z. The control is a Fanuc 0i-TF and the machine weighs 3,500 kg (7,716 lb). No tailstock, C-axis or sub-spindle appears in the listed figures.
Full Specifications
| Parameter | Value |
|---|---|
| Chuck Size | 10 in (254 mm) |
| Maximum Bar Capacity | 78 mm (3.07 in) |
| Maximum Turning Diameter | 300 mm (11.81 in) |
| Maximum Turning Length | 500 mm (19.69 in) |
| Max Spindle Speed | 4,000 RPM |
| Spindle Motor Power | 15 kW (20 hp) |
| Spindle Torque Max | 250 Nm (184 ft-lb) |
| Spindle Bore | 78 mm (3.07 in) |
| Tooling System | Gang-tool flat slide |
| Live Tooling | Optional |
| Workholding | Collet-ready, 10 in hydraulic chuck |
| X-Axis Travel | 200 mm (7.87 in) |
| Z-Axis Travel | 500 mm (19.69 in) |
| Rapid Traverse X | 20 m/min (787 ipm) |
| Rapid Traverse Z | 24 m/min (945 ipm) |
| CNC Control | Fanuc 0i-TF |
| Machine Weight | 3,500 kg (7,716 lb) |
Specifications compiled from manufacturer literature and industry references. Not independently verified against a published spec sheet — confirm with the manufacturer or an authorised dealer before making a purchasing decision.
Strengths & Limitations
Strengths
- 78 mm (3.07 in) spindle bore and bar capacity for large bar and tube
- 15 kW (20 hp) and up to 250 Nm (184 ft-lb) at the spindle
- Collet-ready workholding together with a 10 in hydraulic chuck
- Gang-tool flat slide with no turret index between tools
Limitations
- Gang tooling shares the 200 mm (7.87 in) X travel between tools, which limits tool count on large parts
- A 4,000 RPM maximum restricts surface speed on smaller diameters
- Live tooling is optional, and no C-axis is listed
- No tailstock is listed for the 500 mm (19.69 in) turning length
Best For
Frequently Asked Questions
01
Maximum bar capacity and spindle bore are both listed as 78 mm (3.07 in). Workholding is listed as collet-ready with a 10 in hydraulic chuck, so bar can be gripped either way. Maximum turning diameter is 300 mm (11.81 in).
02
No. The tooling system is listed as a gang-tool flat slide, with tools mounted in a row. The table gives no tool count. On a machine with 200 mm (7.87 in) of X travel, the number of usable tools depends on part diameter and tool spacing.
03
The spindle is listed at 15 kW (20 hp) with a maximum torque of 250 Nm (184 ft-lb) and a maximum speed of 4,000 RPM. The duty rating and the speed at which torque peaks are not stated.
04
Live tooling is listed as optional. The table has no driven-tool speed, no C-axis row and no sub-spindle, so a base machine is for turning only. Confirm what a specific machine carries before planning drilled or milled features.
Videos

MachineryValues Inc

Dale Quint
Community Discussions
Troubleshooting and problem-solving
Links to community discussions. Summaries are editorial — visit the original thread for full context.
More from Hardinge
Other CNC Lathes / Turning Centers
Akira Seiki SL25

Nakamura-Tome SC-200II
Mazak QT-Ez 10MY
Monforts RNC 500